


In the core process of aluminum profile production, the extrusion press is undoubtedly the most critical piece of equipment. Like the heart of the entire production line, it shapes aluminum ingots into profiles of various cross-sectional shapes under immense pressure.
The efficiency, stability, and long-term operation of an extrusion press directly impact product quality and corporate profits.
Basic knowledge of the aluminum extrusion press
An aluminum extrusion press is a heavy-duty machine that uses high pressure to force a heated aluminum billet through a shaped die, producing long, continuous profiles with a specific cross-section. The extrusion press mainly consists of three parts: the mechanical part, the hydraulic part, and the electrical part.
The mechanical part includes the base, prestressed frame tension column, front crossbeam, and movable crossbeam; the hydraulic system includes the main cylinder, side cylinders, and locking cylinder; the electrical part includes the power supply cabinet, operating panel, and PLC programmable controller.
The aluminum extrusion press is the core equipment in any profile production line, whether it is a used aluminum extrusion press or a newly installed system.
Working principles of direct and indirect extrusion presses
Direct extrusion machine
Among various extrusion processes, direct extrusion is the most widely used for aluminum and AlMgSi (6xxx) alloys, which involves no lubrication and the use of sleeves.
The die has no tapered inlet and no radial rays at the inlet end, and is firmly clamped within the press. In the container, the billet and die are preheated before extrusion begins.
A traction machine pushes a billet, or a billet connected to a more advanced press, which alternately pushes the preheated billet into the extrusion assembly, thus sealing the container at the other outlet end.
The billet is then extruded, making it firmly in contact with the container’s interior, continuously forming in the same direction as displacement occurs.
Since direct extrusion is well-suited for aluminum, billet preparation is relatively simple. Producing billets with anodic corrosion resistance is not difficult. The extrusion process is not challenging, and it can be rapidly quenched once it leaves the die. The diameter of the circumferential ring can reach 80% of the container diameter.
In a typical direct extrusion press, such as a 1000T or 1450T aluminum extrusion press machine, the billet moves relative to the container wall, generating friction.
Indirect extrusion press
In indirect extrusion, the tool is fixed to a hollow, stationary core, its end advancing along with the container, pushing the preheated billet towards the apparatus. Thus, extrusion first occurs at the core and a small section at the tail before exiting the pressure zone.
Unlike direct compression, indirect extrusion has no friction between the billet and the container wall, reducing traction by 25%–30% and extrusion pressure by 70%.
Indirectly extruded billets can be much larger than those from direct extrusion; the circumferential dimensions are limited by the internal diameter of the hollow core, resulting in a scrap rate less than half that of direct extrusion.
Throughout the extrusion process, mechanical properties and dimensions are more uniform, the pressure in the container is less intense, and the extrusion speed is much higher than in direct extrusion.
On the other hand, manual control is more difficult, and the risk of damaging the extruded surface is higher. Indirect extrusion was originally used for alloys with poor extrudability.

Core technology differences: Direct extrusion press vs. indirect extrusion press
Friction and heat
Direct Extrusion: The billet presses against the wall of the container. Friction increases. There is more frictional heating. There is a greater temperature variation.
Indirect extrusion: There was much reduced friction between the billet and the container wall. Thus, there was low friction heat generation and easy temperature control.
Temperature differences and unstable friction conditions are two common factors that can contribute to uneven surface marks, die lines, and exit temperatures, particularly at higher extrusion rates.
Stable billet temperature, achieved through a reliable aluminum billet heating furnace, is critical to controlling friction and surface quality.
Scrap rate and billet utilization rate
Direct extrusion is inherently designed to produce scrap at its ends. Indirect extrusion typically offers higher billet utilization due to more uniform flow conditions and different metal behavior. In some cases, indirect extrusion can achieve scrap rates that are less than half that of direct extrusion, depending on conditions and setup.
For plants aiming to reduce costs per ton, the difference in scrap rates alone is significant—especially in large-scale production.
Improving billet utilization directly reduces scrap generation and repeated remelting, which in turn minimizes magnesium ingot burn-off and stabilizes alloy composition.
Cross-sectional size limitations and equipment limitations
Indirect extrusion has some limitations that direct extrusion does not: the geometry of the punch and die limits the maximum cross-sectional size, equipment availability is lower in many areas, and die changes and operation can be more complex in some press designs.
Direct extrusion is generally more suitable for a wider range of profile geometries, including complex hollow profiles, and is the default choice for many “high-mix” plants.
Quick Summary: Direct vs Indirect Extrusion
Direct extrusion offers high flexibility and wide profile capability, making it suitable for high-mix production. Indirect extrusion reduces friction and stabilizes metal flow, resulting in improved billet utilization, lower energy consumption, and more consistent quality for demanding applications.
Direct extrusion:
As shown in the figure, at the start of extrusion, the required pressure rapidly increases to its peak value, known as the breakthrough pressure. Once flow begins, the pressure decreases, and steady-state extrusion continues.
The extrusion pressure reaches its minimum when the loaded billet is almost completely consumed, and then rises sharply as the remaining billet is compacted. The remaining unextruded billet, called billet or waste, accounts for 5% to 15% of the billet.

Indirect extrusion:
In contrast to direct extrusion, the die presses the billet onto the die, rather than pressing the billet against the die. A hollow plunger is attached to the die, compressing the aluminum billet and forcing it to flow.
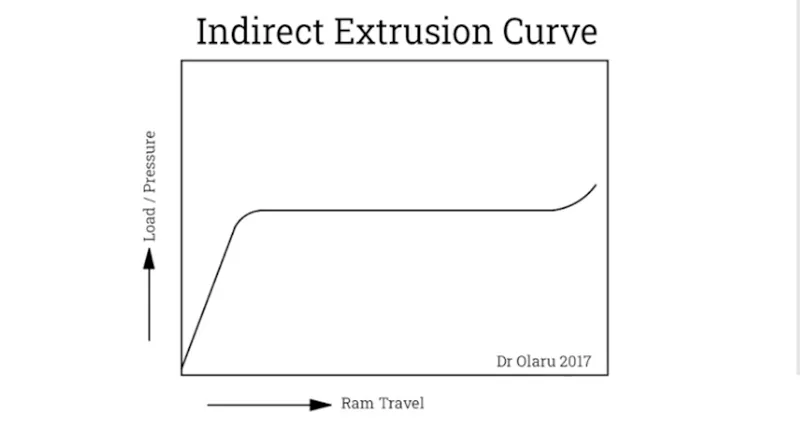
The direction of metal flow is opposite to the direction of plunger travel. Regarding the resulting friction, there is no friction between the billet and the extruder cavity because there is no relative displacement between the billet and the cavity. The effect of this lack of initial friction is described by the pressure-displacement curve shown in the figure below.
As shown, the required pressure only rises to the steady-state extrusion pressure. In many industrial applications, indirect extrusion has been shown to be more energy-efficient than direct extrusion due to reduced friction and a more stable extrusion force profile.
Despite this advantage, indirect extrusion cannot replace direct extrusion. This is because a hollow plunger is required, which is weaker than a solid press. This limits the load that can be used to compress the billet. Therefore, this process is only suitable for producing extrudates with small cross-sections.
Product quality comparison
The quality difference is not absolute; both methods can produce high-quality extrusions, but each method has its own advantages.
Surface quality and finishing rate
Because indirect extrusion reduces heat generated by friction and stabilizes flow, it typically results in a more consistent surface finish.
Hydro’s product marketing also emphasizes that indirect extrusion can provide a more consistent grain structure and better tolerances, thereby helping to improve machinability and finishing results.
Nonetheless, indirect extrusion requires more stringent surface quality from billets. Industry norms stipulate that surface defects, contaminants, or improper billet preparation can lead to issues in surface quality or the formation of depressions, thereby emphasizing the importance of billet cleaning and finishing processes.
Surface quality is influenced not only by the extrusion method but also by the aluminum extrusion die and billet surface preparation.
Consistency of mechanical properties and microstructure
Indirect extrusion provides more stable temperature and load conditions, which can improve the uniformity of grain structure and mechanical properties throughout the extrusion process.
This does not mean that direct extrusion cannot meet stringent specifications, but when you are pursuing the extremes (thin walls, high precision, high surface finish requirements), indirect extrusion can reduce performance fluctuations.
Proper die treatment using a nitriding furnace can significantly extend extrusion die life and reduce operating costs.
Size control
Dimensional stability is affected by a variety of factors, such as die design, cooling, drawing machine control, correction machine, and quenching strategy, but extrusion stability is crucial.
Indirect extrusion has lower friction and more stable conditions, making it easier to maintain tight dimensional tolerances over long production periods.
Maintenance and operating costs
Mold wear and container life
The higher friction in direct extrusion increases wear factors: vessel liner wear, higher thermal cycling counts, increased die stress during high-intensity operations, and a higher risk of thermal cracking.
Indirect extrusion typically reduces frictional heat generation and mitigates certain wear mechanisms, thereby extending vessel life and stabilizing die condition. Industry media reports on the same project indicate that its performance targets are critical to operations.
According to publicly reported industry projects, a newly commissioned 3,000-ton, 12-inch indirect extrusion press achieved up to a 36% productivity increase and a 9% reduction in material consumption, highlighting the potential efficiency gains of indirect extrusion in large-scale applications.
Operating costs
Indirect extrusion requires more stringent process control: billet preparation (cleanliness, deburring, temperature consistency),
more rigorous alignment and die operation, experienced operators, and maintenance procedures. Manual control of indirect extrusion is more challenging, and improper management can increase the risk of surface damage.
Therefore, discussions of operating costs should include training, consistency, and process capability, not just electricity costs.
Application scenarios
Choose a direct extrusion press when you require the following:
- Wide versatility for a variety of profiles**
- Frequency of die changes and high-variety production
- Sufficient market supply (new and used extrusion presses, spare parts, local service)
- Complex shapes for which your team already has aluminum extrusion line/process experience
For building materials (doors and windows), general industrial profiles, and many plants, direct extrusion is often the practical default choice because uptime and flexibility are more important than minor improvements in billet utilization.
Consider using an indirect extrusion press when you require the following.
For building materials (doors and windows), general industrial profiles, and many plants, direct extrusion is often the practical default choice because uptime and flexibility are more important than minor improvements in billet utilization.
Consider using an indirect extrusion press when you require the following.
capabilities:
- Consistent surface finish is a key performance indicator.
- Tight tolerances and machinability are critical (precision bars/strips, high-end industrial profiles).* Energy and scrap costs are major drivers.
- Your billet quality and preparation processes are robust enough to avoid surface contamination issues.
- You have a stable, repeatable product portfolio, and process optimization can yield significant returns.
The investment patterns of leading manufacturers indicate that indirect extrusion technology is gaining increasing traction in areas where productivity, materials efficiency, and sustainability are strategic priorities.

FAQ
1. Is indirect extrusion always better than direct extrusion?
No. Indirect extrusion offers advantages in friction reduction and consistency, but direct extrusion remains more versatile and suitable for complex and large cross-section profiles.
2. Does indirect extrusion reduce scrap?
In many cases, yes. Reduced friction and more uniform metal flow can significantly improve billet utilization and lower scrap rates, depending on process control and billet quality.
3. Can existing plants switch from direct to indirect extrusion?
Indirect extrusion requires specific press structures and cannot be achieved by simple modification. The choice should be made at the stage of equipment investment.
How to choose a suitable extrusion press
Starting with profiles
If the main product line is standard profiles and profiles are frequently changed, direct extrusion is preferred.
If the product line is stable, requires a high surface finish, and has strict tolerances, indirect extrusion is more attractive.
Determine production needs
If tonnage is limited, the lower friction/more stable extrusion pressure of indirect extrusion may help increase production capacity. If the defect rate is high (surface streaks, anodizing waste), indirect extrusion may improve consistency, but only if the billet preparation process is improved.
Calculate total cost
Includes:
- Scrap and docking losses (material utilization rate)
- Cost per ton of mold (lifespan + maintenance)
- Electricity cost per ton
- Downtime and maintenance costs
- Surface finish yield (rework and customer claims)
Actual local service situation
Even the best extruders can fail commercially if spare parts, die support, and experienced maintenance personnel are unavailable. Direct extrusion molding technology has advantages due to its widespread application in many markets.
Choosing the right aluminum extrusion press requires evaluating not only tonnage, but also long-term operating cost and product mix.
Direct extrusion and indirect extrusion are not a matter of superiority or inferiority, but rather different engineering solutions. The advantages of direct extrusion lie in its versatility, availability, and wide applicability.
The advantages of indirect extrusion lie in reduced friction, more stable process conditions, material utilization, and consistency, especially in demanding applications. This is supported by the actual industrial investments and performance targets of major manufacturers.
We are a professional aluminum machinery manufacturer and serve aluminum plants worldwide. We specialize in providing complete plant design and layout solutions, and offer high-quality aluminum extrusion production equipment.
If you are planning to invest in aluminum extrusion presses or optimize your existing extrusion production line, our technical team will provide you with professional guidance based on actual production data and industry best practices. Please feel free to contact us anytime.
Author Note
This article is written by an engineering team with long-term experience in aluminum extrusion press selection, production line design, and plant optimization. Our work covers direct and indirect extrusion systems, billet heating, die management, and downstream processing across aluminum plants worldwide.